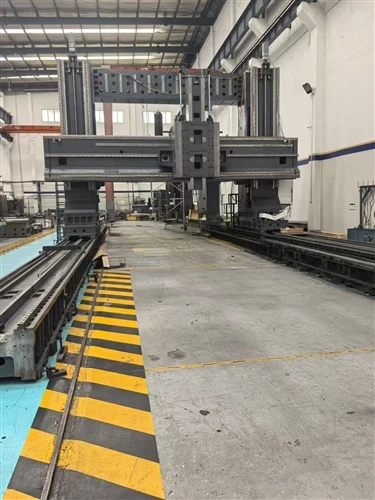
Before using the machine tool for machining, it must be checked to ensure it is in normal operating condition. This check includes using individual blocks, checking feed rate overload, machine tool locking function, and no-load operation. Before operating the machine tool, carefully check the input data to ensure it is correct and that the feed rate is suitable for the operation to be performed. When using the tool compensation function, carefully check the direction and compensation amount. The CNC and PMC parameters are set by the manufacturer and generally do not need to be changed. If changes are necessary, understand the function of the parameter first. After powering on, do not touch any buttons on the MDI panel until the position display or alarm appears. Ensure the coordinate system is correct and pay attention to the correctness of the imperial and metric settings. When programming polar coordinate insertion programs or normal direction control programs, pay special attention to the speed of the rotary axes. An inappropriate program will cause the rotary axis speed to be too high, and the resulting centrifugal force may cause the fixture to detach from the workpiece. When the axis under constant surface speed control reaches the origin of the workpiece coordinate system, the spindle speed will become very high; therefore, the maximum permissible speed must be specified. If the stroke detection fails, no alarm will be triggered even if the stroke exceeds the limit, which may pose a danger. A tool holder interference check is required. After starting the machine tool, a reference position return should be performed. When operating manually, the feed rate factor must be correctly selected. Operators must strictly adhere to the above procedures; otherwise, unexpected actions may occur, damaging the tool, machine tool, workpiece, or causing personal injury.
 English
- English
- Français
- Deutsch
- 日本語
- Italiano
- Español
- Português
- русский
- Gaeilgenah Éireann
- 한국어
- Latviešu
- Bai Miaowen
- اردو
- हिंदी
- Cymraeg
- عربي
- Eesti
- Polski
- українська
- magyar
- עברית
- Türkçe
- Kreyòl Ayisyen
- suomi
- slovenščina
- dansk
- Việt Nam
- slovenčina
- Nederlands
- România limbi
- íslenska
- Norsk
- Melayu
- Čeština
- فارسی
- Indonesia
- Ελληνικά
- Svenska
- O'zbek
- বাংলা
- ไทย
- hrvatski
- Srbija jezik (latinica)
- bosanski
- Malti
- Català
- Български
- Lietuvių